The dairy homogenization machine is a critical piece of equipment in modern dairy processing, designed to transform the physical properties of milk through high-pressure processing. This milk homogenizer reduces fat globule size from the natural 3-5 microns to less than 1 micron, creating a stable, uniform mixture where fat particles remain suspended rather than rising to the surface. The result is dairy products with smoother texture, better mouthfeel, improved nutritional absorption, and significantly extended shelf life. Whether you’re operating a small yogurt shop or a large-scale dairy processing facility, understanding the role of homogenization in dairy production is essential for achieving consistent, high-quality products that meet consumer expectations.
High-Pressure Technology: 15-25 MPa | SUS 304 Construction | Two-Stage Homogenization | 200-5000L/hr Capacity
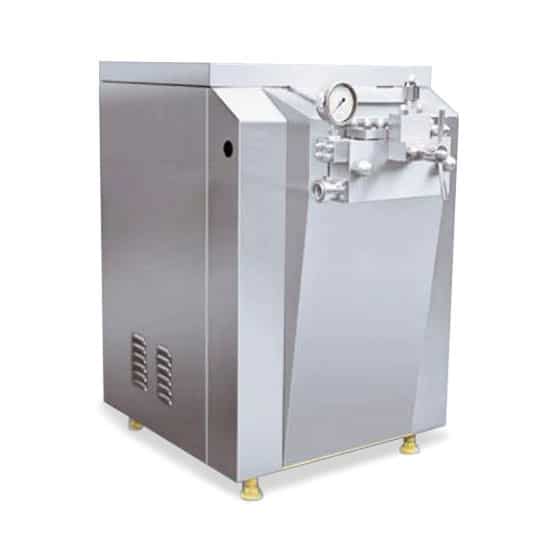
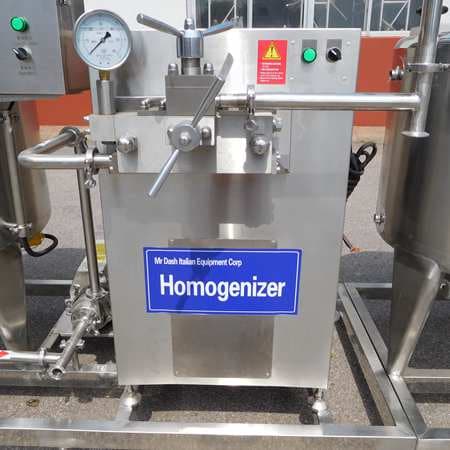
High-pressure milk homogenizer machine for dairy processing with stainless steel construction
Why Homogenization is Essential in Dairy Processing
In untreated milk, fat globules are relatively large and have a tendency to rise to the surface due to density differences - this is the cream layer you may have observed in untreated milk. This natural separation presents several challenges for dairy processors: inconsistent product texture, unappealing appearance, and reduced shelf stability. The milk homogenizer solves these problems by mechanically reducing fat globule size and creating an emulsion where fat remains evenly distributed throughout the product.
The Science of Fat Globule Size Reduction
Unhomogenized milk fat globules typically range from 1-15 microns in diameter, with an average around 3-5 microns. These larger globules rise to the surface due to buoyancy (Stokes’ Law), forming a visible cream layer within 24-48 hours.
Homogenization reduces this size to less than 1 micron through high-pressure mechanical processing. At this size, the fat globules remain permanently suspended and do not separate, creating a stable emulsion that can last for weeks or months.
Impact on Yogurt Production
For yogurt production, homogenization is particularly important because it directly impacts the final texture, appearance, and quality of the yogurt:
Homogenization Effect
Without Homogenization
With Homogenization
Fat Distribution
Uneven, rises to surface
Uniformly distributed
Texture
Grainy, inconsistent
Smooth, creamy
Whey Separation
Visible after 24 hours
Minimal or none
Shelf Life
7-14 days
14-21 days
Fermentation Consistency
Variable batch quality
Consistent results
Understanding Homogenization Technology
Single-Stage vs. Two-Stage Homogenization
The homogenization process can be configured as single-stage or two-stage, each with distinct advantages:
Configuration
First Stage
Second Stage
Best For
Single-Stage
15-25 MPa
None
Standard yogurt, fresh milk
Two-Stage
20-25 MPa
3-5 MPa
Greek yogurt, high-fat products, premium dairy
Two-stage homogenization is essential for high-fat dairy products because:
Prevents Re-coalescence: After the first stage breaks down fat globules, the second stage at lower pressure prevents them from recombining
Improves Emulsion Stability: Creates more stable bonds between fat globules and proteins
Better Texture Development: Critical for thick, creamy Greek yogurt and premium products
Why Pressure Matters: Technical Deep-Dive
The relationship between homogenization pressure and fat globule size follows predictable patterns:
Pressure
Average Globule Size
Resulting Texture
Best Application
10 MPa
1.5-2.0 microns
Light, pourable
Drinking yogurt
15 MPa
1.0-1.5 microns
Smooth, medium body
Standard yogurt
20 MPa
0.5-1.0 microns
Thick, creamy
Premium yogurt
25 MPa
< 0.5 microns
Very thick, premium
Greek yogurt, labneh
The Science: Cavitation and Shear Effects
The high-pressure homogenizer works through two main physical effects:
Cavitation Effect: When milk accelerates through the homogenizer gap at high pressure, static pressure drops below fat’s saturated vapor pressure, causing cavitation (microbubble formation). The collapse of these bubbles creates localized shock waves that mechanically crush fat globules. This effect is particularly effective for breaking down large fat aggregates.
Shear Effect: High-velocity flow through narrow homogenizing valve gaps generates powerful shear forces (fluid shear). These shear forces deform, elongate, and ultimately pulverize fat globules into fine particles. The combination of cavitation and shear effects ensures complete homogenization.
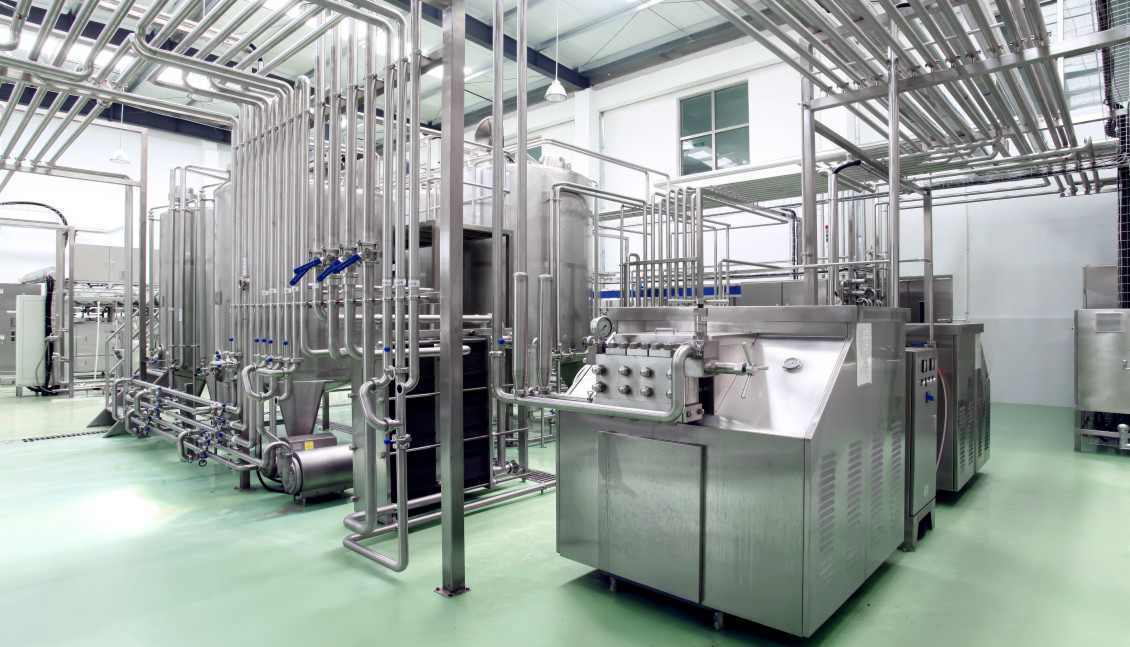
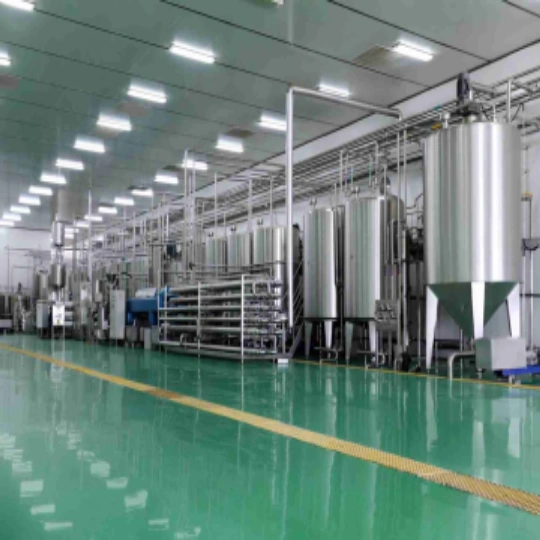
Milk homogenizer integrated in yogurt production line showing processing flow from preheating to sterilization
Types of Homogenization Equipment
Modern dairy processing facilities utilize several types of homogenization equipment:
Type
Pressure Range
Capacity
Best Application
Price Range
High-Pressure Homogenizer
15-25 MPa
200-5000L/hr
Commercial yogurt
$8,000-$50,000
Two-Stage Homogenizer
20-25 + 5 MPa
500-10000L/hr
Premium dairy, Greek yogurt
$15,000-$80,000
Ultrasonic Homogenizer
Acoustic
Up to 100L/hr
Laboratory, research
$5,000-$20,000
Inline Homogenizer
10-20 MPa
1000-20000L/hr
Continuous production
$20,000-$100,000+
For most commercial yogurt production applications, the high-pressure homogenizer with two-stage configuration offers the best balance of efficiency, effectiveness, and cost.
Shuliy vs. Competitors: Technical Comparison
Feature
Shuliy Homogenizer
Typical Competitor
Pressure Range
15-25 MPa
10-20 MPa
Two-Stage Design
Standard
Often single-stage
Plunger Material
Ceramic-coated
Standard steel
Valve Material
Tungsten carbide
Stainless steel
Temperature Control
Built-in heating
External required
Pressure Stability
+/- 0.5 MPa
+/- 1-2 MPa
Continuous Operation
24/7 capability
8-12 hours
Motor Efficiency
IE3 premium efficiency
IE2 standard
Noise Level
< 85 dB
90-95 dB
Warranty
2 years
1 year
Key Technical Advantages
Superior Valve Technology: Our homogenizing valves are manufactured from tungsten carbide, providing 3x longer service life compared to standard stainless steel valves. The precision-machined valve seats ensure consistent pressure distribution across the homogenizing gap.
Advanced Seal Design: Proprietary seal technology prevents pressure leakage and extends maintenance intervals by 40%.
Premium Motor Efficiency: IE3 premium efficiency motors reduce energy consumption by 10-15% compared to standard motors, significantly lowering operating costs.
Role in Yogurt Production
In the yogurt production line, the homogenizer requires milk preheating to approximately 55C for optimal fat globule membrane elasticity. A milk preheating machine is positioned before the homogenizer to ensure proper temperature before processing. After homogenization, the milk proceeds to sterilization, creating the optimal foundation for yogurt fermentation.
Optimal Processing Parameters
Parameter
Recommended Value
Effect of Deviation
Preheating Temperature
50-60C
Below 45C: poor homogenization
Homogenization Temperature
55-70C
Above 70C: protein denaturation
First Stage Pressure
20-25 MPa
Lower: incomplete homogenization
Second Stage Pressure
3-5 MPa
Absent: re-coalescence risk
Fat-to-Casein Ratio
0.2g casein/g fat
Affects texture stability
Homogenization quality depends on several interconnected factors: temperature, pressure, and the fat-to-casein ratio (ideally 0.2g casein per gram of fat). When these parameters are optimized, the result is milk that ferments evenly, produces yogurt with superior texture, and maintains quality throughout its shelf life.
Structure & Components
The milk homogenizing machine is a three-plunger reciprocating pump consisting of precision-engineered components:
Core Components
Component
Function
Maintenance Interval
Main drive shaft
Converts motor rotation to reciprocating motion
12 months
Transmission belt
Transfers power to pump assembly
6 months
Plungers (3x)
Generates high-pressure flow
3-6 months
Suction valves
Controls milk entry to cylinder
6-12 months
Discharge valves
Controls milk exit under pressure
6-12 months
Homogenizing valve
Primary homogenization site
3-6 months
Pressure gauge
Monitors operating pressure
12 months
seals and gaskets
Maintains pressure integrity
3-6 months
Three-Plunger Design Advantages
The three-plunger configuration provides several advantages over single or dual-plunger designs:
Continuous Flow: One plunger is always in the discharge stroke, ensuring uninterrupted production
Reduced Pulsation: Three overlapping pressure cycles minimize pressure fluctuations
Balanced Operation: Equal load distribution across three plungers reduces wear
Higher Efficiency: More complete milk processing with each stroke cycle
Operating Guidelines for Optimal Results
Temperature Management
Always preheat milk to 50-60C before homogenization. At this temperature range, fat globule membranes are most elastic and can be broken down most effectively.
Below 45C: Fat is too solid for proper emulsification
Above 65C: Protein denaturation may occur
Optimal range: 55-70C for most yogurt applications
Pressure Optimization
For standard yogurt production, operate at 15-20 MPa in the first stage and 3-5 MPa in the second stage. Higher pressures (up to 25 MPa) may be used for high-fat products or when producing premium-grade yogurt with extra smooth texture.
Flow Rate Control
Maintain consistent flow rates through the homogenizer. Sudden pressure changes can damage valves and reduce homogenization efficiency. Use variable frequency drives to adjust flow rates for different batch sizes.
Pre-Filtration Requirement
Always filter raw milk before homogenization to remove debris, hair, and other particles that could clog the homogenizing valve or damage plungers. Install a 100-200 mesh filter upstream of the homogenizer.
Quality Verification Methods
Visual Inspection
Signs of proper homogenization include:
No visible cream layer after 24 hours of storage
Uniform white appearance without yellowish tint
Smooth, consistent texture
Microscopic Analysis
Regular testing with a microscope to observe fat globule size is the most reliable indicator:
Proper homogenization: < 1 micron average
Under-homogenized: 1-3 microns with visible variation
Poor homogenization: > 3 microns with cream separation
Stability Testing
Perform shelf stability tests:
24-hour test: No visible separation
7-day test: Minimal whey separation acceptable
14-day test: Should maintain smooth texture
Economic Analysis: ROI of Homogenization
Cost Comparison
Factor
Without Homogenizer
With Homogenizer
Savings
Product Value
Base price
Premium pricing (+15-20%)
$0.15-0.20/cup
Shelf Life
7-14 days
14-21 days
50% extension
Wastage
3-5%
< 1%
2-4% of production
Customer Complaints
Frequent
Rare
Immeasurable
Payback Calculation
For a 1000L/day yogurt operation:
Equipment investment: $20,000-35,000
Annual production: 300,000 liters
Value increase from premium product: $45,000/year
Reduced wastage savings: $6,000/year
Energy cost addition: $2,000/year
Net annual benefit: $49,000
Payback period: 5-7 months
Maintenance Schedule
Daily Operations
Check oil levels, listen for unusual noises, and verify pressure gauge readings before each production run.
Weekly Maintenance
Inspect seals and gaskets for wear, clean homogenizing valves, and check belt tension.
Monthly Service
Replace worn seals, inspect suction and discharge valves, and calibrate pressure sensors.
Annual Overhaul
Complete inspection of plungers, valve seats, and bearings; replace all wear parts; verify mechanical integrity.
Technical Specifications
Parameter
Specification
Equipment Type
High-pressure homogenizer
Main Structure
Three-plunger reciprocating pump
Material
SUS 304 stainless steel
Optimal Temperature
55-70C
Operating Pressure
15-25 MPa
First Stage
15-25 MPa adjustable
Second Stage
3-5 MPa adjustable
Capacity
200-5000L/hr
Motor Power
7.5-45 kW depending on model
Applications
Dairy, beverages, biotechnology, pharmaceuticals
Frequently Asked Questions
Q: What is the difference between single-stage and two-stage homogenization?
A: Single-stage homogenization uses one homogenizing valve at high pressure. Two-stage homogenization adds a second valve at lower pressure (typically 3-5 MPa) after the first stage. The second stage prevents fat globule re-coalescence and is especially important for high-fat dairy products like cream or yogurt, ensuring long-term stability and consistent texture.
Q: Can homogenization replace pasteurization?
A: No, homogenization and pasteurization serve different purposes. Homogenization is a mechanical process that reduces fat globule size, while pasteurization is a heat treatment that destroys pathogenic bacteria. Both processes are typically used in yogurt production for different purposes.
Q: How do I know if my homogenizer is working properly?
A: Signs of proper homogenization include: no visible cream layer after 24 hours of storage, smooth texture in finished yogurt, and consistent results batch to batch. Regular testing with a microscope to observe fat globule size (should be less than 1 micron) is the most reliable indicator of homogenization efficiency.
Q: What maintenance is required for the homogenizer?
A: Daily inspection includes checking oil levels and pressure readings. Weekly maintenance includes inspecting seals and cleaning valves. Monthly service includes replacing worn seals and calibrating sensors. Annual overhaul includes complete inspection of plungers and bearings.
Related Products
For complete dairy processing solutions, explore our complementary equipment:
Yogurt Production Line
- Complete turnkey solution integrating homogenization as a key processing stage
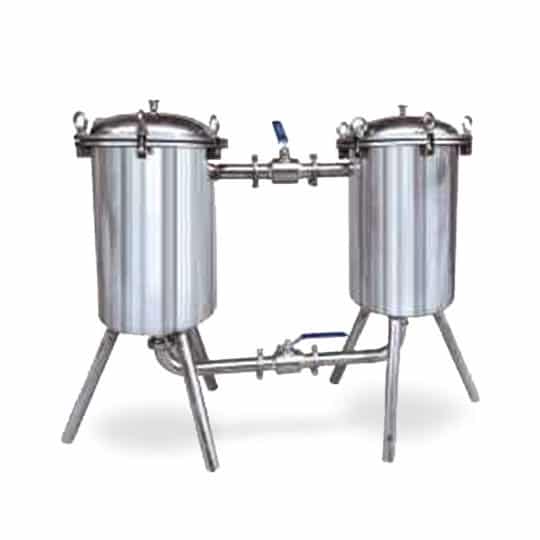
The milk filter (duplex filter) is the industrial filtering device for all kinds of liquid product filtration, and it is especially practical for the filtering of fruit juices, drinks, milk, and other liquid foods.
Professional automatic yogurt production line manufacturer. Custom capacity from 200L to 5000L per day. ISO & CE certified. Factory direct price. Get free quote within 24 hours!
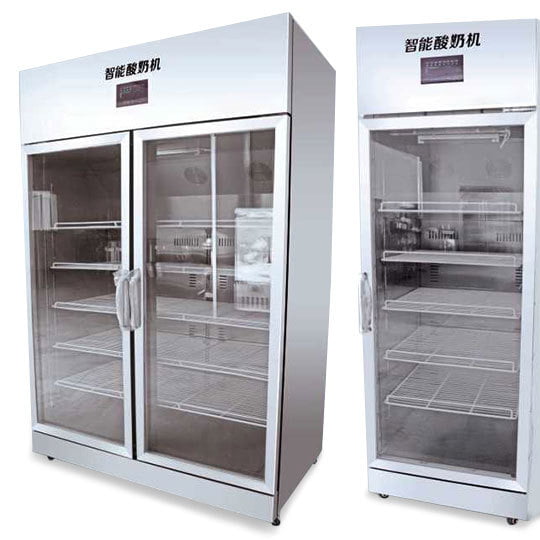
Commercial yogurt fermentation maker for sale. Single and double chamber options with automatic temperature control. Perfect for yogurt shops and cafes. Factory direct pricing. Get your free quote today!
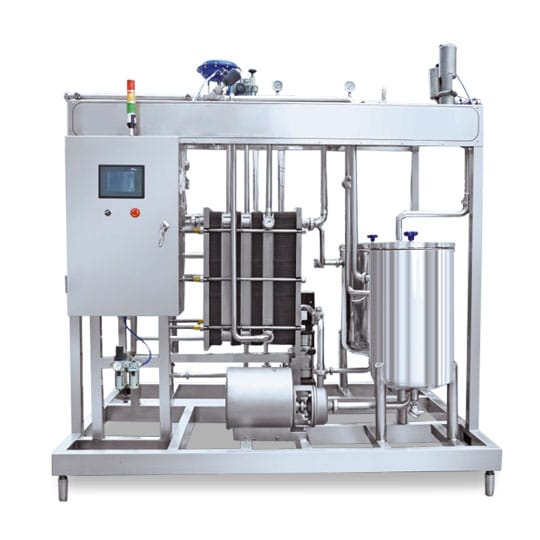
Professional milk pasteurizer machine for yogurt and dairy processing. HTST pasteurization technology. 200L-5000L capacity. CE certified. Best price from manufacturer!